

How Deep Is Deep Enough? Engagement Length Rules for Inserts in Aluminum
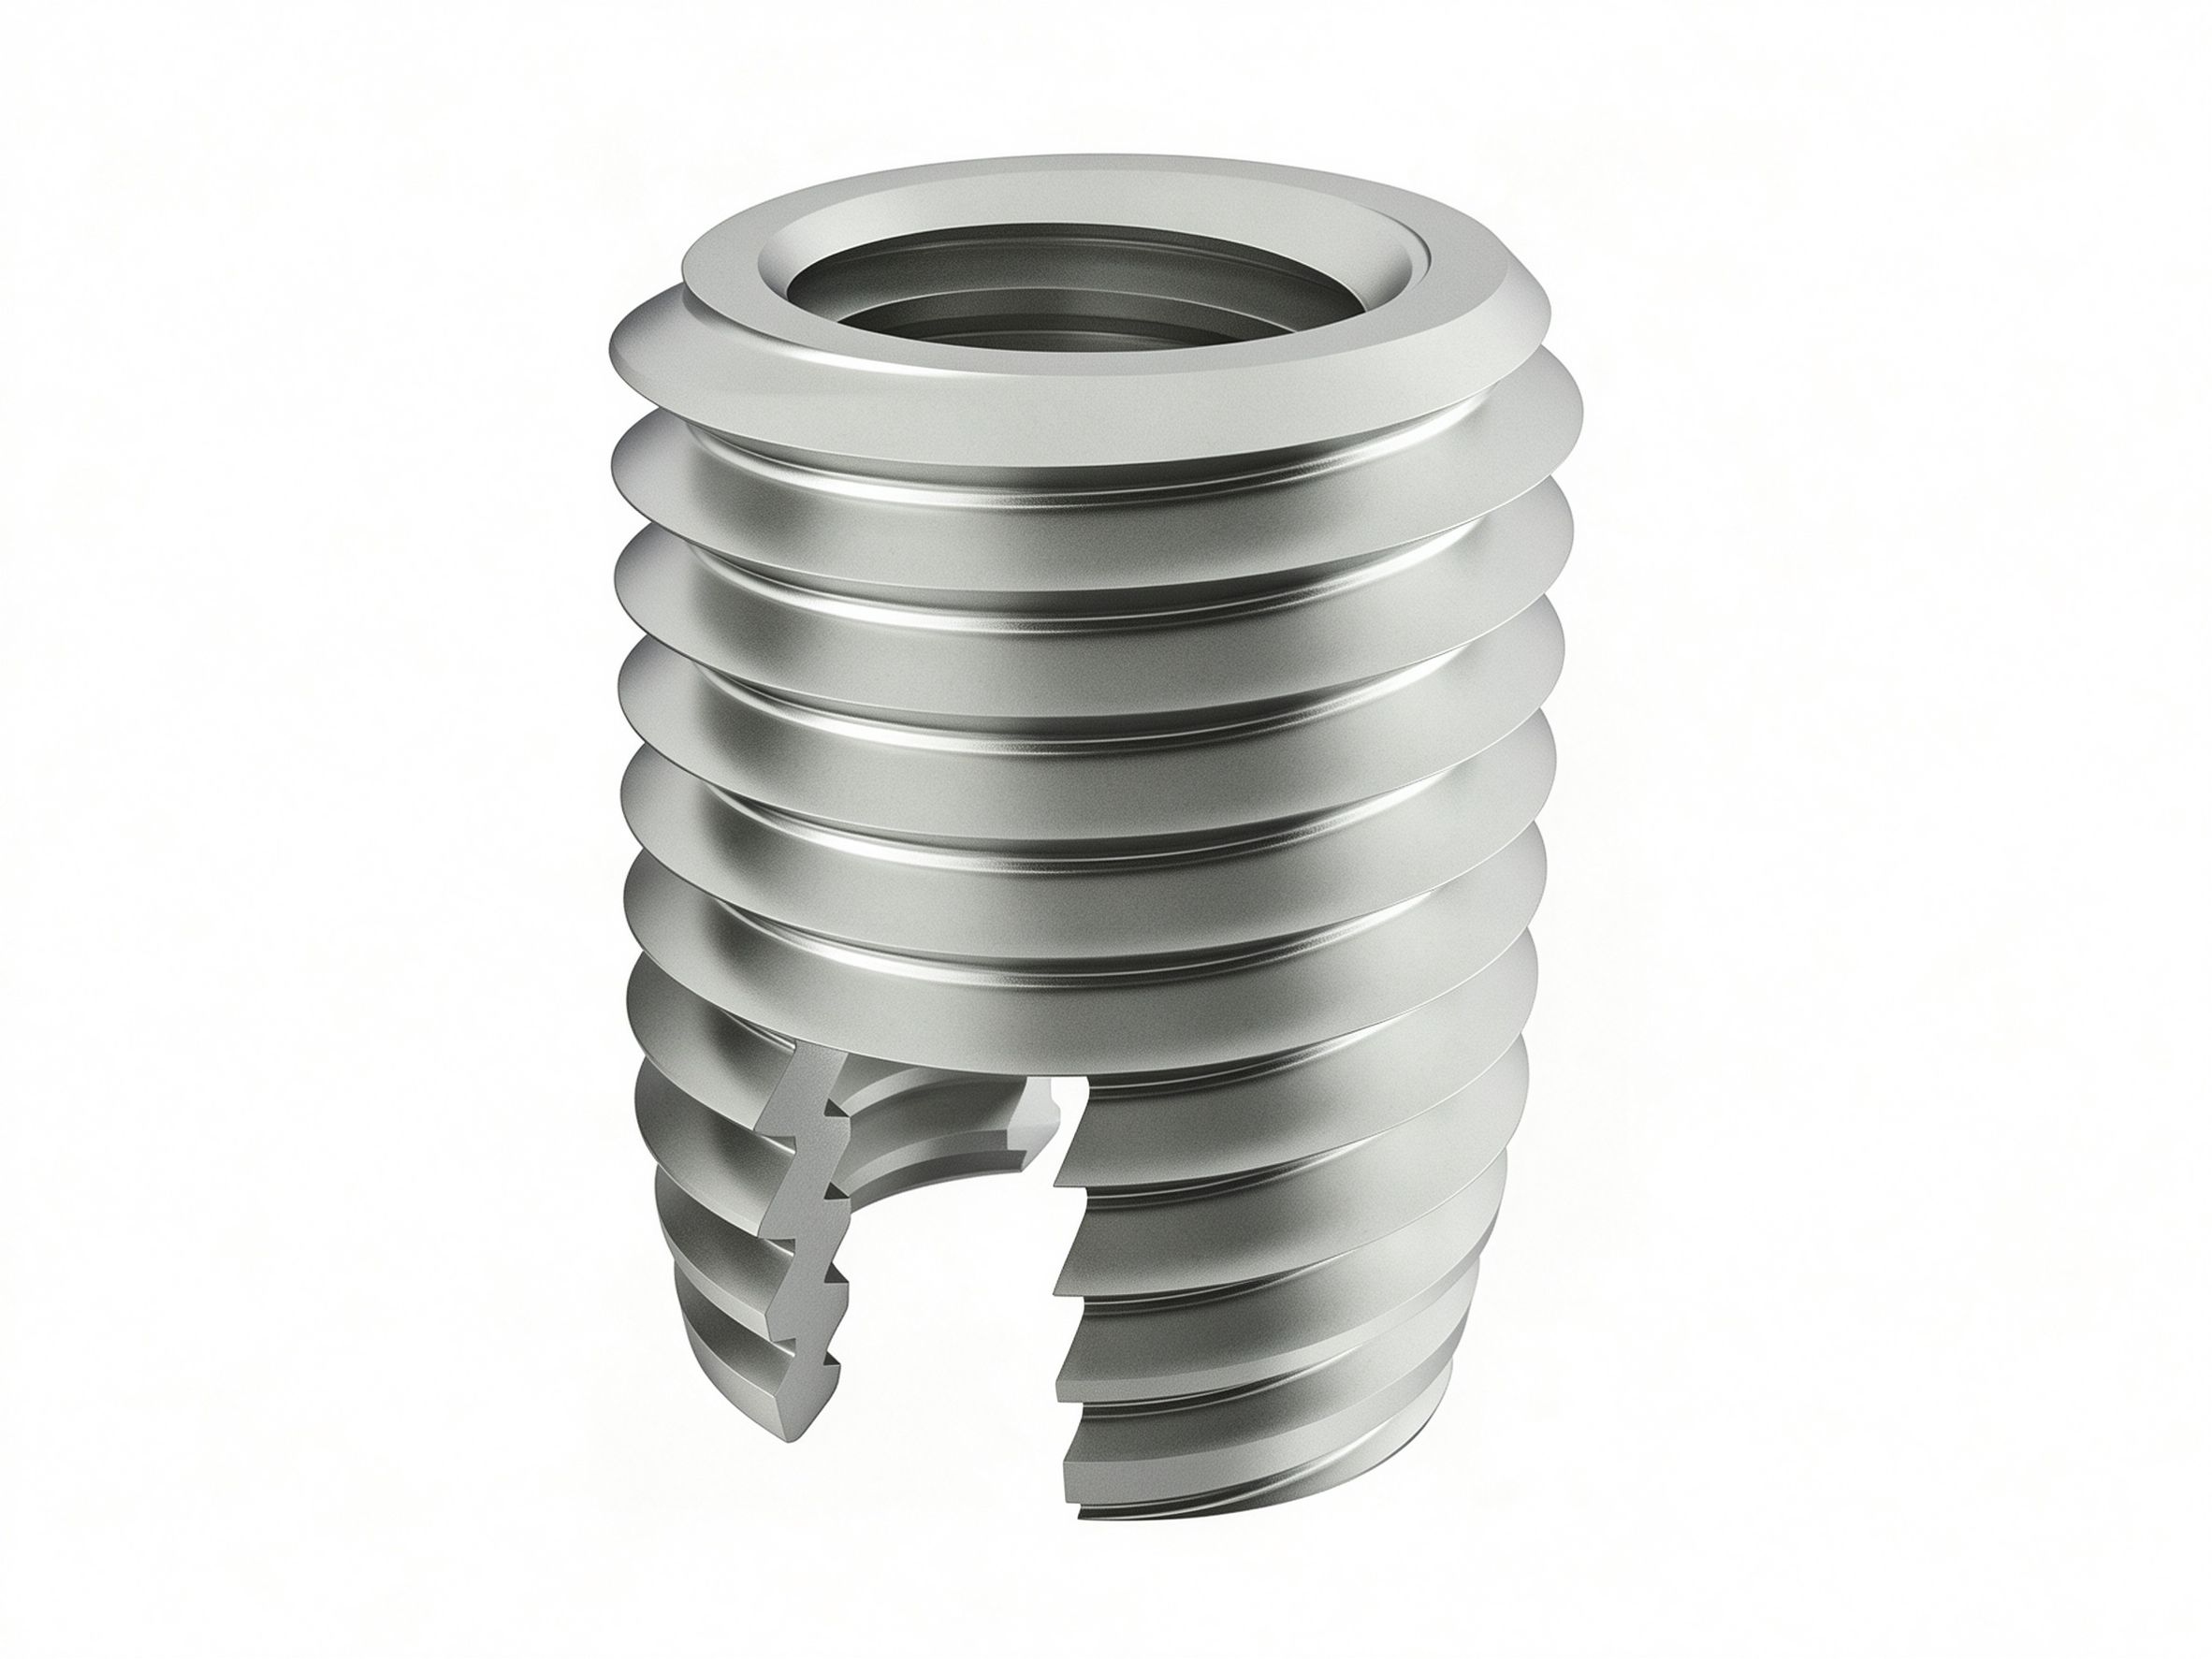
Bolted joints fail at their weakest link. In steel, that is almost always the bolt. In aluminum, the parent thread strips first unless engagement is designed deliberately.
Bottom line: for most Light-Alloy Die Castings applications the decision comes down to load, environment and assembly method — the Light-Alloy Die Castings guide walks through the selection.
The 1.5D baseline
For a steel bolt in aluminum without an insert, the classic rule is 2.0–2.5 times bolt diameter of engaged thread. With a steel wire thread insert installed, the effective shear area multiplies and 1.0–1.5D usually reaches bolt-strength parity. That reduction is the core economic argument for inserts: shorter bosses, smaller castings, lighter housings.
Where the baseline bends
- Thermal cycling (EV drive units): add 0.5D because differential expansion relaxes preload.
- Repeated assembly: gage wear, not static strength, limits life — spec insert classes tested for 15+ assembly cycles.
- Blind holes: chip space at the bottom steals 1–2 pitches; design depth accordingly.
Verify by pull-out test
Rules of thumb start the design; testing finishes it. A simple axial pull-out fixture on three castings from different mold cavities will expose cavity-to-cavity porosity variation that no calculation predicts. Toprecision publishes strip-out torque data for its insert range in A360, ADC12 and 6061 parents, and can support joint qualification with sample kits for your own pull-out rigs.
Wire thread insert selection at a glance
| Insert type | Thread material | Best for | Temperature limit |
|---|---|---|---|
| Standard free-running | 304 stainless | General aluminum/ magnesium housings | ~300°C |
| Screw-locking (prevailing torque) | 304 stainless | Vibration-prone joints | ~300°C |
| Inconel X-750 | Inconel | Aerospace, engine hot zones | ~750°C |
| Keensert (solid bushing) | Steel/zinc-plated | Repeated assembly, heavy load | ~400°C |
Need help selecting the right fastener material?
Toprecision cold-heads and CNC-turns fasteners in steel (4.6–12.9), stainless 304/316/410, aluminum 6061/7075, titanium Grade 5 and engineering plastics. Send the service environment and load requirement — we will recommend the material and grade with tensile test data. Request material selection support.
