

Wire Thread Insert Installation: Tap Sizes, Preload and the Mistakes That Cost Most
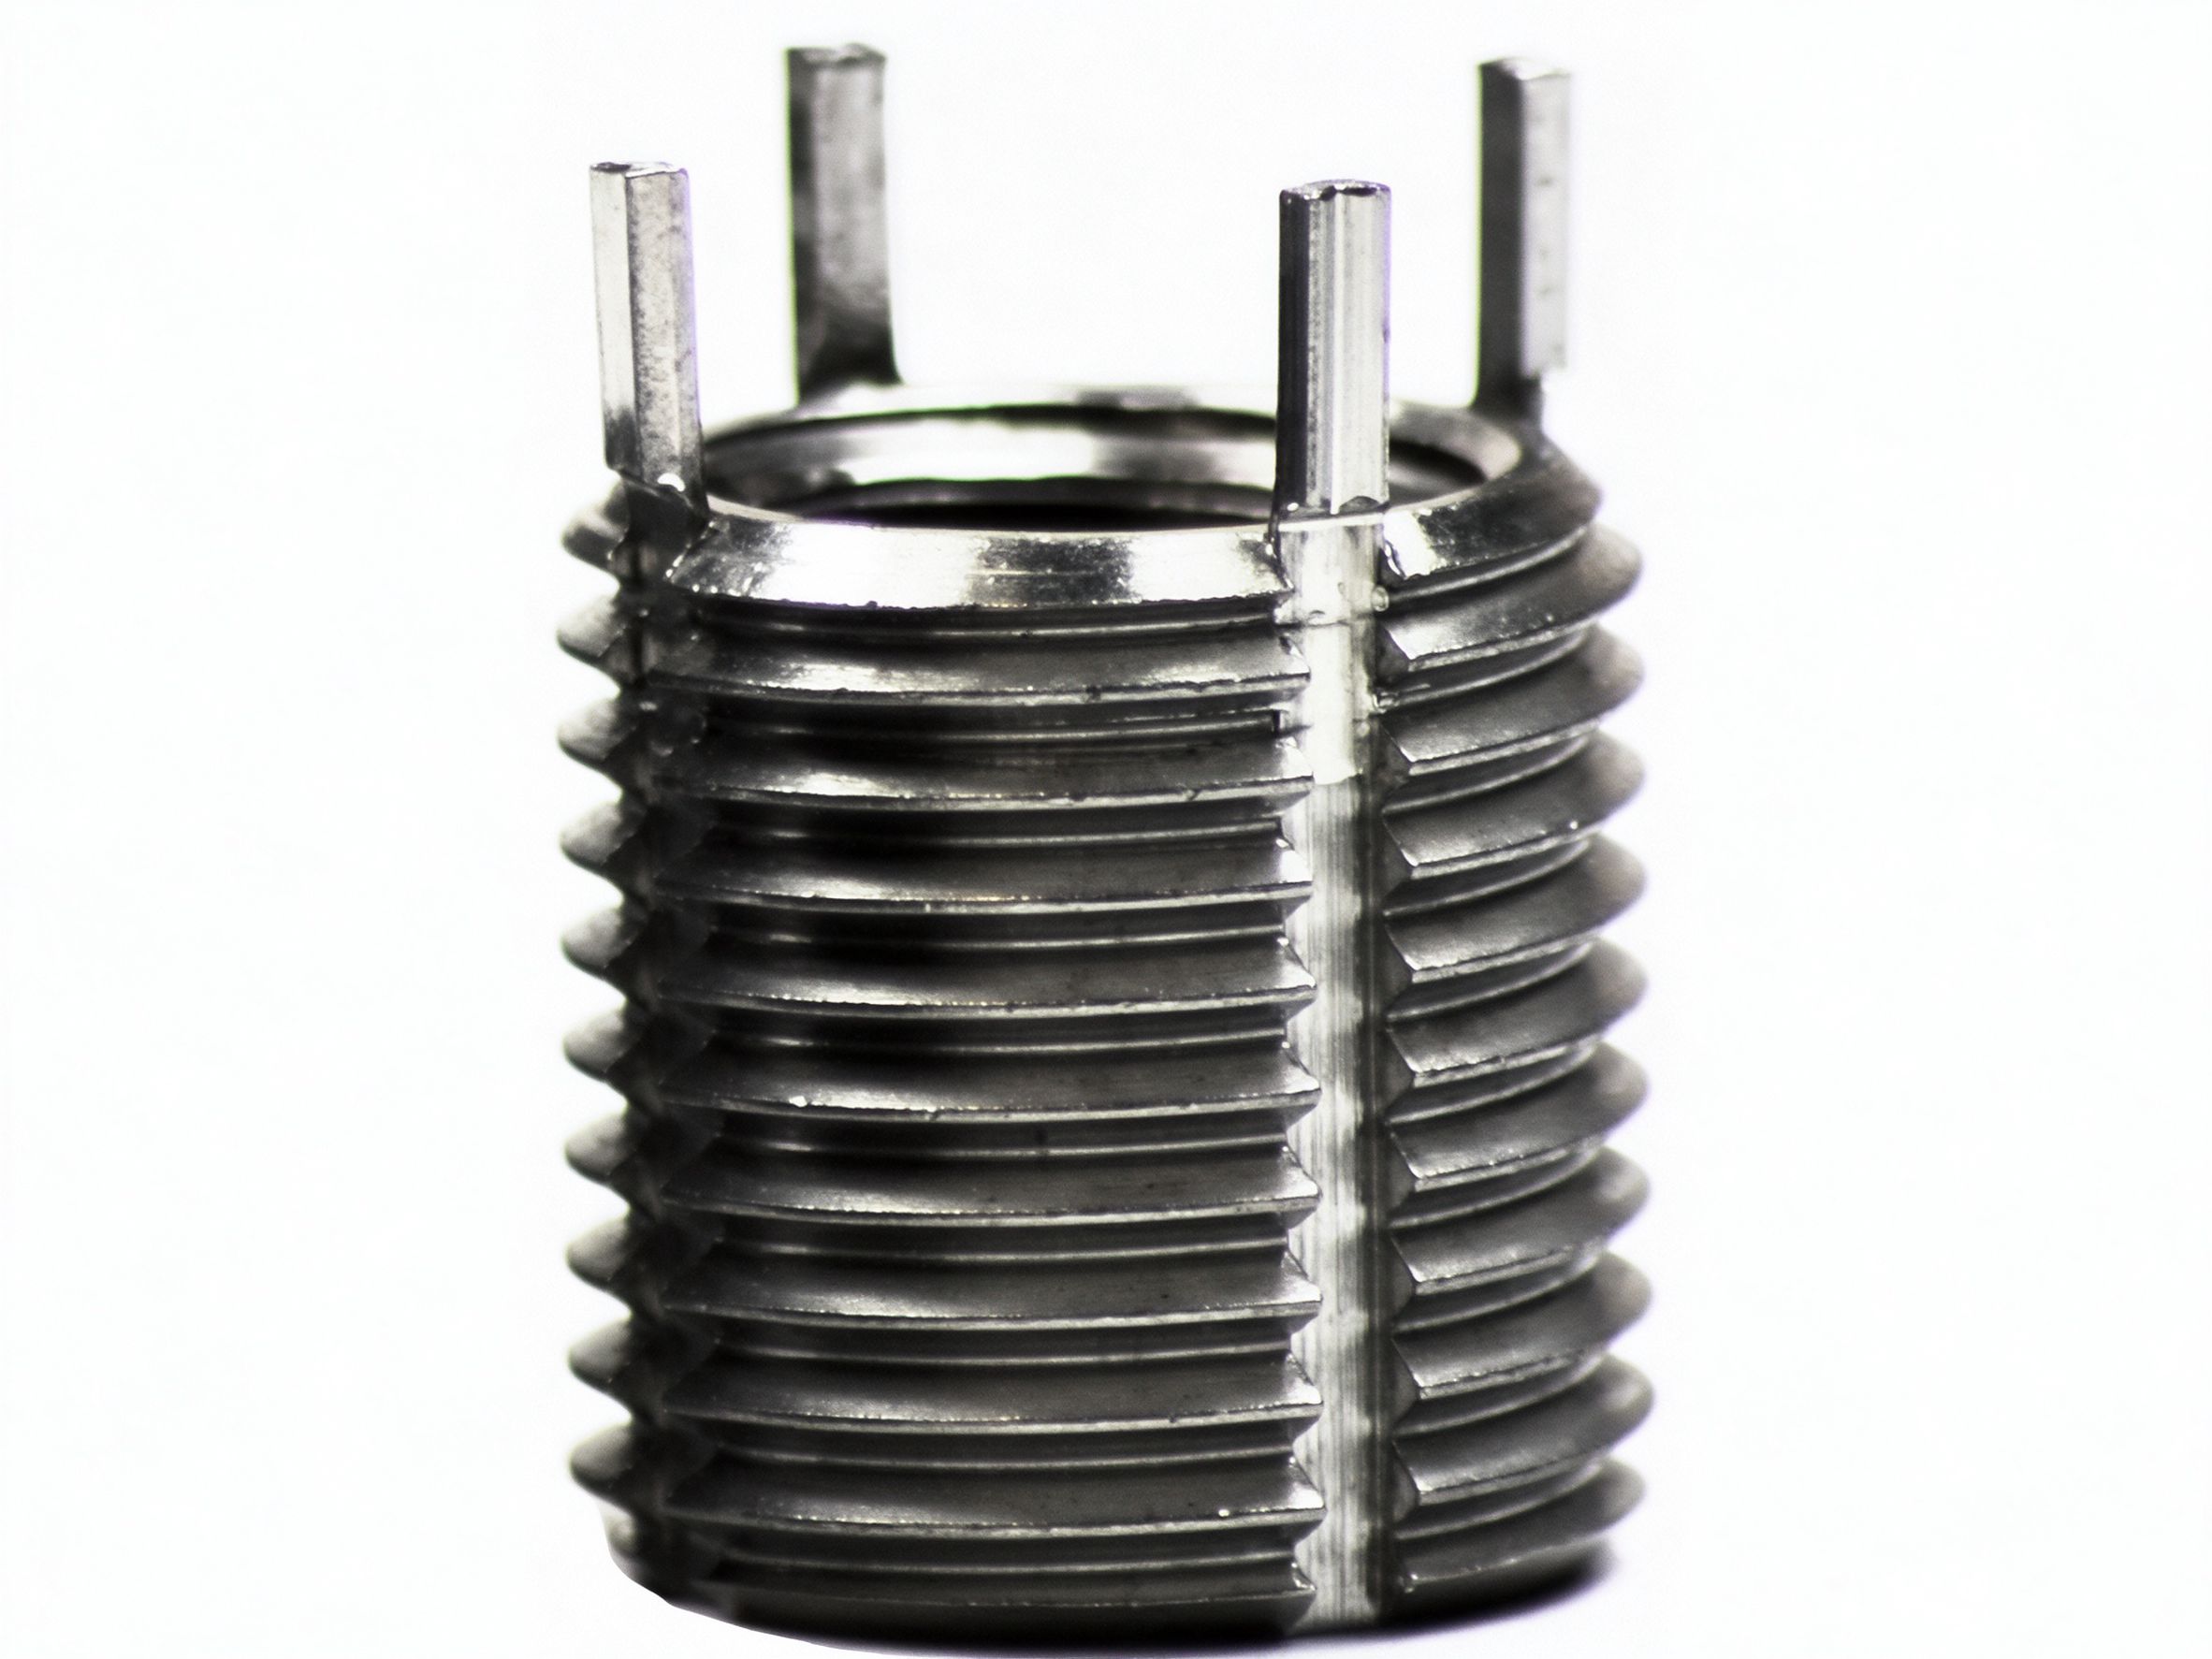
Wire thread inserts promise aerospace-grade threads in soft metals, but most field failures trace back to a handful of installation errors made before the insert is even wound in.
Bottom line: for most Thread Inserts applications the decision comes down to load, environment and assembly method — the Thread Inserts guide walks through the selection.
Start with the STI tap, not the bolt
An insert seat is cut with a Screw Thread Insert (STI) tap, whose major diameter is oversized to accept the coiled wire. Using a standard tap of the same nominal size is the single most common mistake: the assembled thread then measures undersized and the screw wrecks the insert on first tightening. Always confirm the tap marking (for example M6x1.0 STI) against the insert part number.
Depth, chamfer and cleanliness
- Drill or tap depth should exceed the insert length by 1.5–2 pitches so the insert Driving Tang seat never bottoms out.
- A 90° countersink chamfer protects the first thread and helps the pre-winder start square.
- Blow out chips and coolant before insertion; trapped chips are a leading cause of false torque readings.
Gage the result, not the intent
Preload depends on the assembled thread, so verify with an STI Go/No-Go gage after installation — a torque wrench confirms friction, not thread geometry. For critical joints, record gage acceptance per hole. Toprecision supplies inserts with matching tap and gage recommendations on every datasheet, so your line can qualify a station once and repeat it for years.
Wire thread insert selection at a glance
| Insert type | Thread material | Best for | Temperature limit |
|---|---|---|---|
| Standard free-running | 304 stainless | General aluminum/ magnesium housings | ~300°C |
| Screw-locking (prevailing torque) | 304 stainless | Vibration-prone joints | ~300°C |
| Inconel X-750 | Inconel | Aerospace, engine hot zones | ~750°C |
| Keensert (solid bushing) | Steel/zinc-plated | Repeated assembly, heavy load | ~400°C |
Need wire thread inserts for your housing?
Toprecision supplies 304/316 stainless and Inconel X-750 wire thread inserts, plus keenserts and self-tapping inserts for aluminum, magnesium and die-cast housings. Send the housing material and thread size — we will supply the tap drill chart, installation torque and sample push-out test data. Request insert engineering support.
