

Thread Rolling vs Thread Cutting: The Strength Difference You Can Measure
Two screws with identical geometry can differ 20–50% in fatigue life depending on how their threads were made. The difference is cold work.
Bottom line: for most Thread Inserts applications the decision comes down to load, environment and assembly method — the Thread Inserts guide walks through the selection.
What rolling does
Thread rolling presses hardened dies against the blank, displacing material into the thread form. Nothing is removed: grains flow along the flank contours, the surface work-hardens, and compressive residual stress develops in the root — precisely where fatigue cracks start. Cut threads, by contrast, sever grains and leave tensile stress and tool marks at the root.
The measurable consequences
- Fatigue strength: rolled threads routinely beat cut ones by wide margins in repeated-load tests.
- Surface finish: rolling leaves smooth flanks — better friction consistency, better torque control.
- Material economy: no chips, faster cycle, cheaper per piece at volume.
When cutting still wins
Very small batches, oversized diameters beyond rolling-machine capacity, and some hard or exotic materials cut more practically than they roll. Blind-hole internal threads below certain sizes are cut because rolling taps cannot handle them. Topprecision rolls threads as standard on its production screws — including its 7-series aluminum bolt line, where the root's compressive layer is a key fatigue asset — and cuts only where volume or geometry demands.
Key specifications at a glance
| Parameter | Typical range | Note |
|---|---|---|
| Thread size range | M1.6–M24 standard, up to M64 special | Custom diameters available |
| Property class | 4.6–12.9 steel, A2-70/A4-80 stainless | Per ISO 898-1 / ISO 3506 |
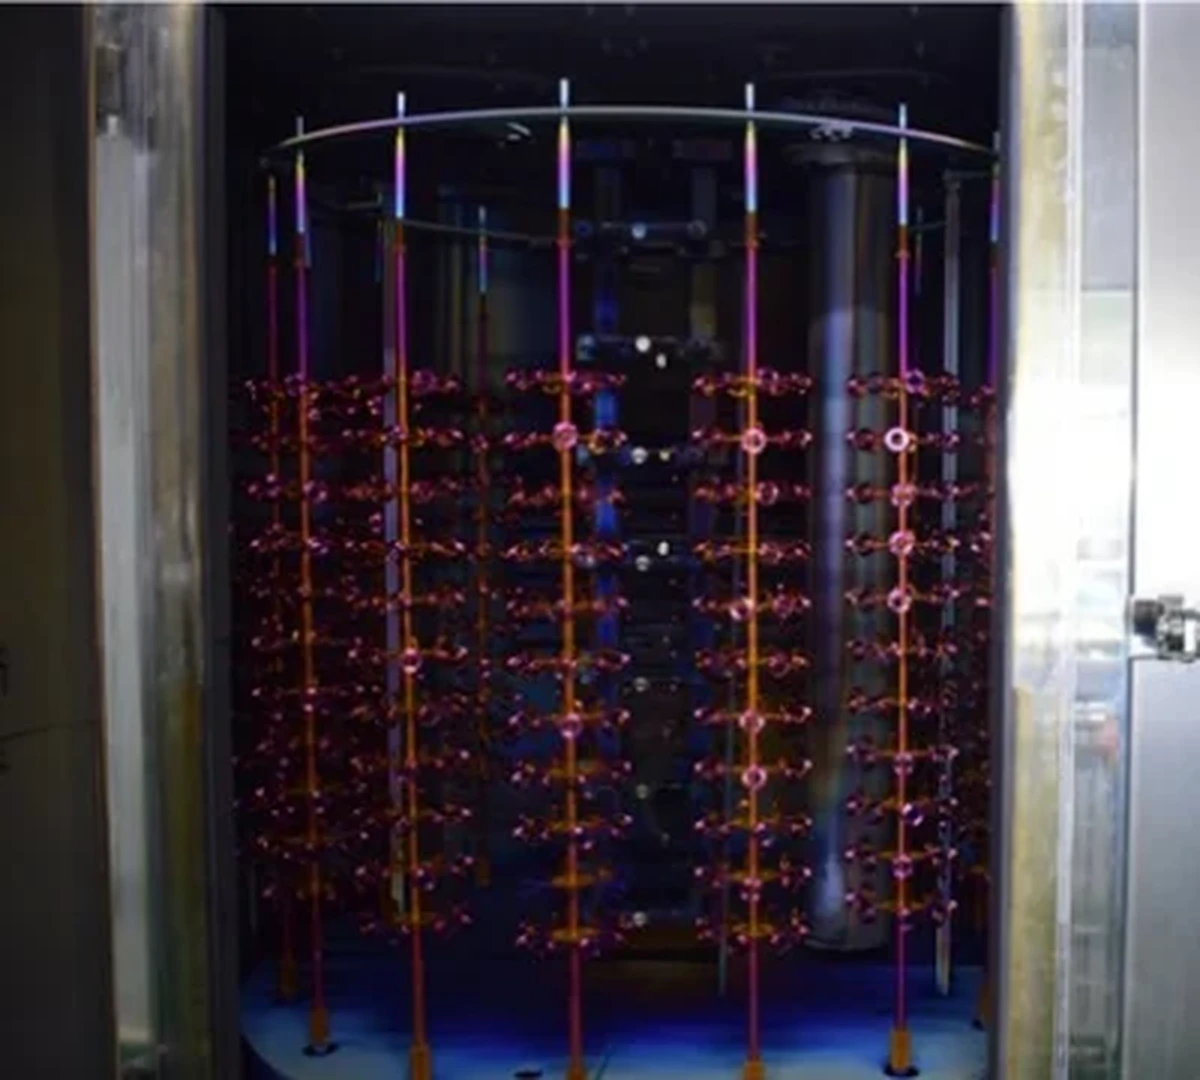
| Surface finish | Zinc, Dacromet, PTFE, DLC, PVD | Matched to service environment |
| Production method | Cold heading + thread rolling | CNC turning for specials |
| Quality standard | ISO 9001, IATF 16949 | Batch traceability |
Need fastener engineering support?
Toprecision manufactures precision fasteners in-house — send the drawing, service environment and annual volume. We will recommend the material, grade, coating and process that match the joint requirement. Request a fastener consult.
